
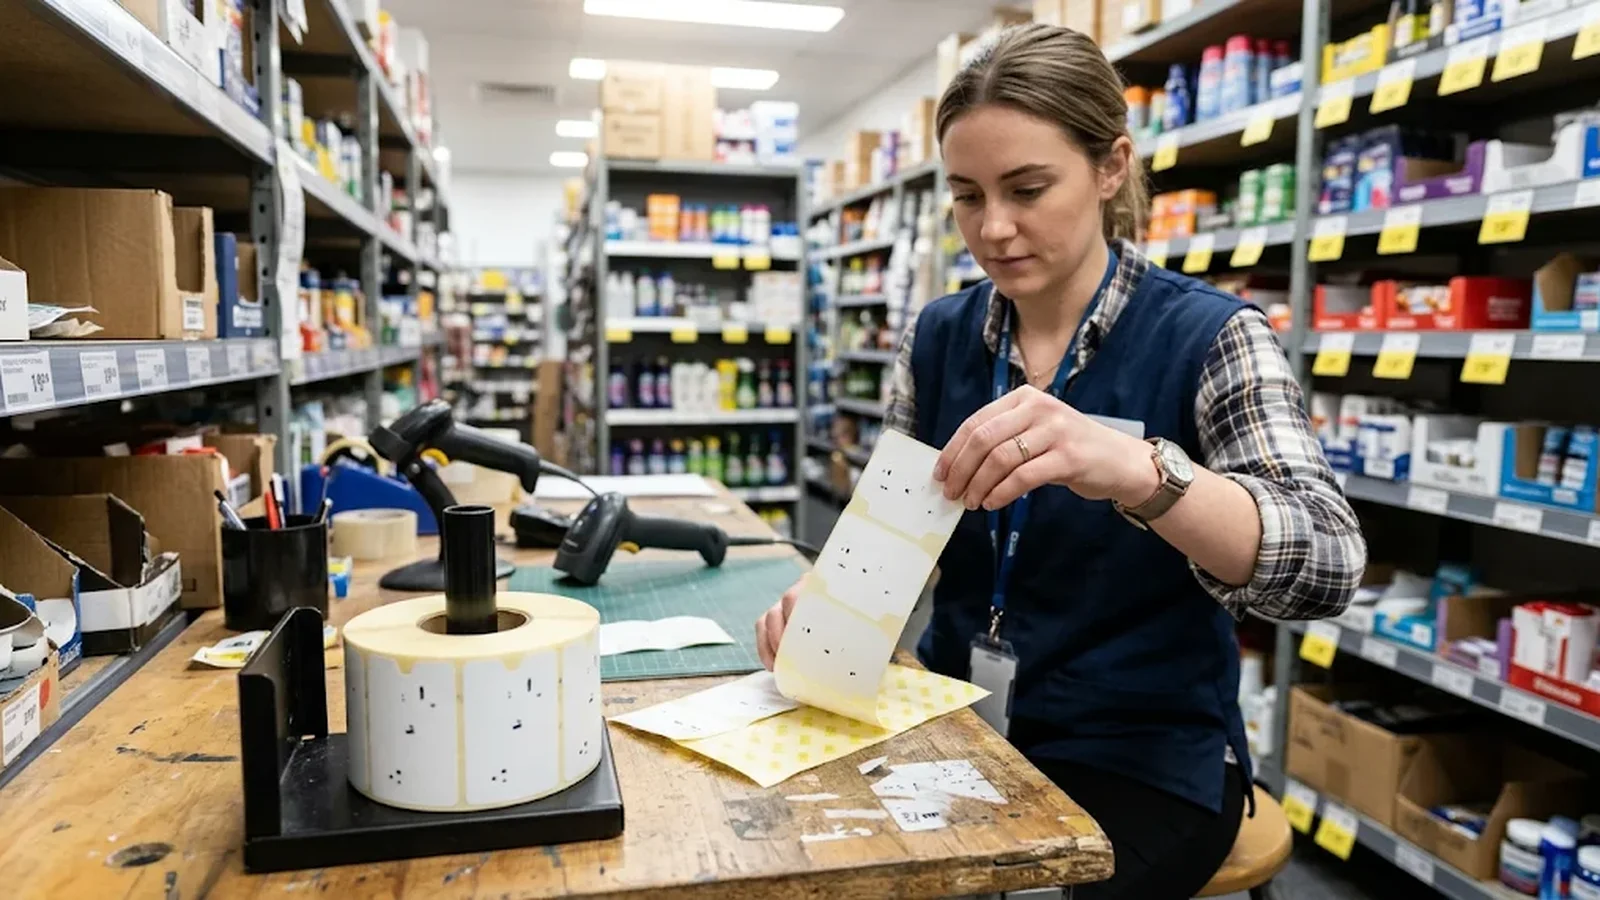
A thermal sticker label is a three-layer laminate: a direct thermal facestock that images without ink, a pressure-sensitive adhesive that bonds the label to the product or shelf, and a release liner that carries the die-cut labels on a roll until application. Buying them well means specifying all three layers plus the cut — facestock grade and whether it is top-coated, adhesive class matched to the surface and service temperature, liner weight and release force, die-cut geometry with gap and web width tolerances, and core size matched to the applicator or dispenser. The failures buyers actually experience are adhesive failures, not print failures: labels lifting on curved or low-energy surfaces, edge ooze in hot containers, or liners that break on the applicator. Those are all specification-controlled properties, and a qualified label stock supplier will quote adhesive, liner and die-cut data alongside the thermal grade instead of selling 'thermal labels' as one undifferentiated item.
Sticker labels are the quiet workhorse of retail consumables: price and shelf stickers, weighing-scale labels, promotional stickers, returned-goods tags — every one a small laminate that has to print cleanly, stick reliably and die-cut without pulling liners apart. When they work, nobody notices; when the adhesive is wrong for the surface, the complaint reaches the supplier long after the container has been paid for.
That is because a thermal sticker label is not one product but three decisions made together: the thermal facestock that carries the image, the pressure-sensitive adhesive that carries the bond, and the release liner that carries the label through converting, transport and application. Each layer has its own specification and its own failure modes, and the interactions between them — adhesive bleed into a thin thermal coat, a liner too weak for high-speed dispensing — are where cheap constructions come apart.
Buyers comparing these specifications can review our top-coated thermal label stock, where facestock, adhesive and liner options are documented per construction before an order is placed, so the three-layer decision is made on data rather than on a single 'thermal labels' price line.
This guide works through each layer in turn — what the facestock grade and top-coat decide, how adhesive classes map to surfaces and temperatures, what liner and die-cut specifications protect applicator performance — and closes with the commercial terms and packing standards that keep a repeat label programme consistent.
- Specify the laminate, not just the paper: facestock grade, adhesive class and liner weight are three separate decisions that interact — quote them together on one specification sheet.
- Adhesive failure, not print failure, is the dominant field complaint: match adhesive class to surface energy, curvature and service temperature before comparing prices.
- Top-coated facestock buys water, oil and abrasion resistance for stickers handled, stacked or refrigerated; non top-coated suits dry, short-life retail duty at lower cost.
- Die-cut discipline protects the applicator: cut depth into the liner, gap width, web width tolerance and roll winding all need stated tolerances, not catalogue defaults.
- Judge the supplier on converting evidence — sample rolls from the actual construction, batch COA/SDS, and packing that protects adhesive and facestock through ocean freight.
Facestock: the thermal grade under the adhesive
The facestock is the thermal paper itself — a base sheet carrying the thermal coating that images under a print head. For sticker constructions the facestock is typically a 55–75 gsm thermal grade, laminated to the adhesive and liner at converting. Grade choice follows the same logic as receipt paper: lighter grades keep cost down and feed well in compact printers, heavier grades add stiffness and a premium hand-feel that matters on shelf-edge and promotional stickers where the label is part of the product's appearance.
The construction decision that matters most is top-coated versus non top-coated. A top-coated facestock adds a protective layer over the thermal coating that resists water, oil, alcohol and plasticiser migration — the difference between a freezer or deli sticker that stays legible for months and one that fades in a fortnight. Non top-coated constructions image equally well and cost less, and are the right choice for dry, short-life duty: price stickers consumed within days, shelf labels in climate-controlled aisles, event and ticketing stickers handled once.
Sensitivity class belongs on the specification too. Facestocks are graded by activation energy and image density, and a mismatch between the label's sensitivity and the printer's head energy produces pale prints that no adhesive can rescue. Ask the supplier to state the sensitivity class and the target image density with the test method, and verify on your own printer before fleet-wide rollout — the print test costs nothing and closes the most common quality gap.
For production volumes, the same construction logic applies to our 75 gsm heavyweight thermal paper, quoted per jumbo roll, slit reel or finished format, for programmes that want a heavyweight paper facestock laminated to a buyer-specified adhesive rather than a stock label construction.
Adhesive: where sticker programmes actually fail
Pressure-sensitive adhesives divide into families, and each family earns its keep on different surfaces. General-purpose acrylic adhesives cover most retail duty on cardboard, glass and high-energy plastics. Hotmelt adhesives bring aggressive initial tack for rough or low-energy surfaces but soften in heat, which makes them wrong for hot cases or sunny storefronts. Removable adhesives trade permanence for clean peel — the right choice for promotional stickers applied to packaging that must not tear on removal. Specialty classes extend the range: deep-freeze adhesives that bond below zero, high-tack formulations for curved surfaces, wash-off adhesives for returnable crates.
Service temperature brackets the choice from both ends. Every adhesive datasheet carries a minimum application temperature and a service temperature range; applying below the minimum means the adhesive never wets the surface, and the label lifts within hours. Buyers shipping into cold chains or hot climates should treat those two numbers as purchase conditions, not datasheet trivia, and should state the destination environment on the enquiry — a label that performs in a temperate warehouse can fail on a winter loading dock.
Surface energy is the other half of the match. Low-energy plastics (PE, PP, some shrink films) resist wetting, and a sticker that bonds happily to glass will lift silently from a plastic tub. The professional habit is to test the actual surface, at the actual application temperature, with the actual adhesive class, before committing volume — three sample rolls and a week of trials buy out the most expensive class of field failure.
| Adhesive class | Best on | Watch for |
|---|---|---|
| General-purpose acrylic | Cardboard, glass, high-energy plastics | Slow bond build on cold surfaces |
| Hotmelt | Rough, low-energy surfaces; fast tack | Softens in heat; edge ooze in hot storage |
| Removable | Promotional stickers on packaging | Reduced permanence; not for cold chains |
| Deep-freeze | Refrigerated and frozen surfaces | Higher cost; verify condensation handling |
| High-tack / curved-surface | Curved containers, difficult plastics | Harder removal; residue on some surfaces |
Liner and die-cut: the specifications applicators feel
The release liner is a glassine or film carrier, typically 40–80 gsm for paper liners, whose job is to release cleanly under the applicator while surviving the tension of high-speed dispensing. Liner too thin and it breaks mid-roll; release force too high and labels stay on the liner; too low and they flag off in transit. Manual-dispenser programmes tolerate wider bands than automated applicators, which need release force specified and verified — a spec the supplier should hold batch to batch, because liner drift shows up as downtime on the packing line, not as a paper complaint.
Die-cut geometry is the second applicator-critical specification. The cut must penetrate the facestock and adhesive fully without scoring the liner (a cut-through liner breaks at speed), and the geometry — label size, corner radius, gap between labels, web width — needs tolerances stated in writing. Gap consistency decides whether the printer's label sensor sees each label edge; a gap drifting out of tolerance produces the 'misaligned print' complaints that are actually die-cut complaints. Roll orientation, winding direction and core size (commonly 25.4 mm or 76.2 mm class) complete the fit-to-machine picture.
Where image life is the deciding factor, our top-coated vs non top-coated guide compares the two constructions on retention, cost and machine behaviour, so facestock and adhesive choices can be made as one documented decision rather than two catalogue lines.
Converters running mixed label and receipt formats should consolidate the specification set: one sheet per SKU covering facestock grade, adhesive class, liner, die-cut geometry, core and winding, revision-controlled, so every repeat order is measured against the same drawing instead of the last shipment's memory.
Qualifying a thermal sticker label supplier
Evidence beats vocabulary. A qualified label stock supplier will send sample rolls converted on the actual production construction — not lab sheets — and will state the adhesive class, service temperature bracket, liner weight and release force with the quotation. Batch documentation should travel with production: COA for the thermal grade, SDS identifying the developer chemistry, and traceability from finished carton back to facestock lot and adhesive batch, so a field complaint can be investigated rather than guessed at.
MOQ in this category is driven by construction changes: each adhesive or liner switch consumes setup, so the minimum reflects the converter's planning honesty. Mixed-SKU programmes can usually consolidate several label formats — different sizes, one adhesive family — into a single production run and a single container, which is where the unit economics of a direct-from-manufacturer relationship become visible against a distribution intermediary.
Packing is a laminate-preservation problem. Adhesives age with heat and humidity, facestocks scuff, and liner edges crush — so cartons need inner barriers, compression strength matched to pallet stacking, and desiccant where climates demand it. Where container planning is the next step in an import programme, our export shipping guide covers pallet standards, moisture-barrier packing and the document set for ocean freight.
Requests that combine several formats can be quoted together; see our custom thermal paper programme for the construction, die and packing options behind each one, quoted per programme rather than per catalogue item.
Qualification shorthand: sample rolls from the actual construction, adhesive class + service temperature stated, liner weight + release force specified, die-cut geometry with tolerances, COA + SDS per batch, carton-to-carton traceability, moisture-barrier export packing.
Frequently asked questions
What is a thermal sticker label?
A three-layer laminate: a direct thermal facestock that prints without ink or ribbon, a pressure-sensitive adhesive that bonds to the surface, and a release liner that carries the die-cut labels on a roll. All three layers — plus the die-cut geometry — need specification, because each carries its own failure modes.
Do thermal stickers need a special printer?
They print in any direct thermal printer matched to the label's width, sensitivity class and die-cut format. The usual requirement is a gap or black-mark sensor setting for label media rather than continuous receipt paper, plus print-head energy suited to the facestock's sensitivity class.
Why do my thermal stickers peel off plastic surfaces?
Almost always an adhesive-surface mismatch. Low-energy plastics such as PE and PP resist adhesive wetting, and cold application temperatures make it worse. Fix it by matching adhesive class to the surface — often a high-tack or specialty acrylic — and testing the actual surface at the actual application temperature before committing volume.
When should I choose top-coated label stock?
Wherever stickers meet moisture, oil, alcohol or abrasion: refrigerated and deli environments, labels handled repeatedly, stickers surviving weeks on the product. Non top-coated constructions are the economical choice for dry, short-life retail duty such as price stickers consumed within days.
What specifications should a label enquiry include?
Label dimensions and shape, thermal facestock grade and construction (top-coated or not), adhesive class with service temperature range, liner type and weight, die-cut gap and web width, roll core and winding, and the packing environment. Suppliers who answer each line with data are manufacturers; suppliers who answer with a price alone are intermediaries.