
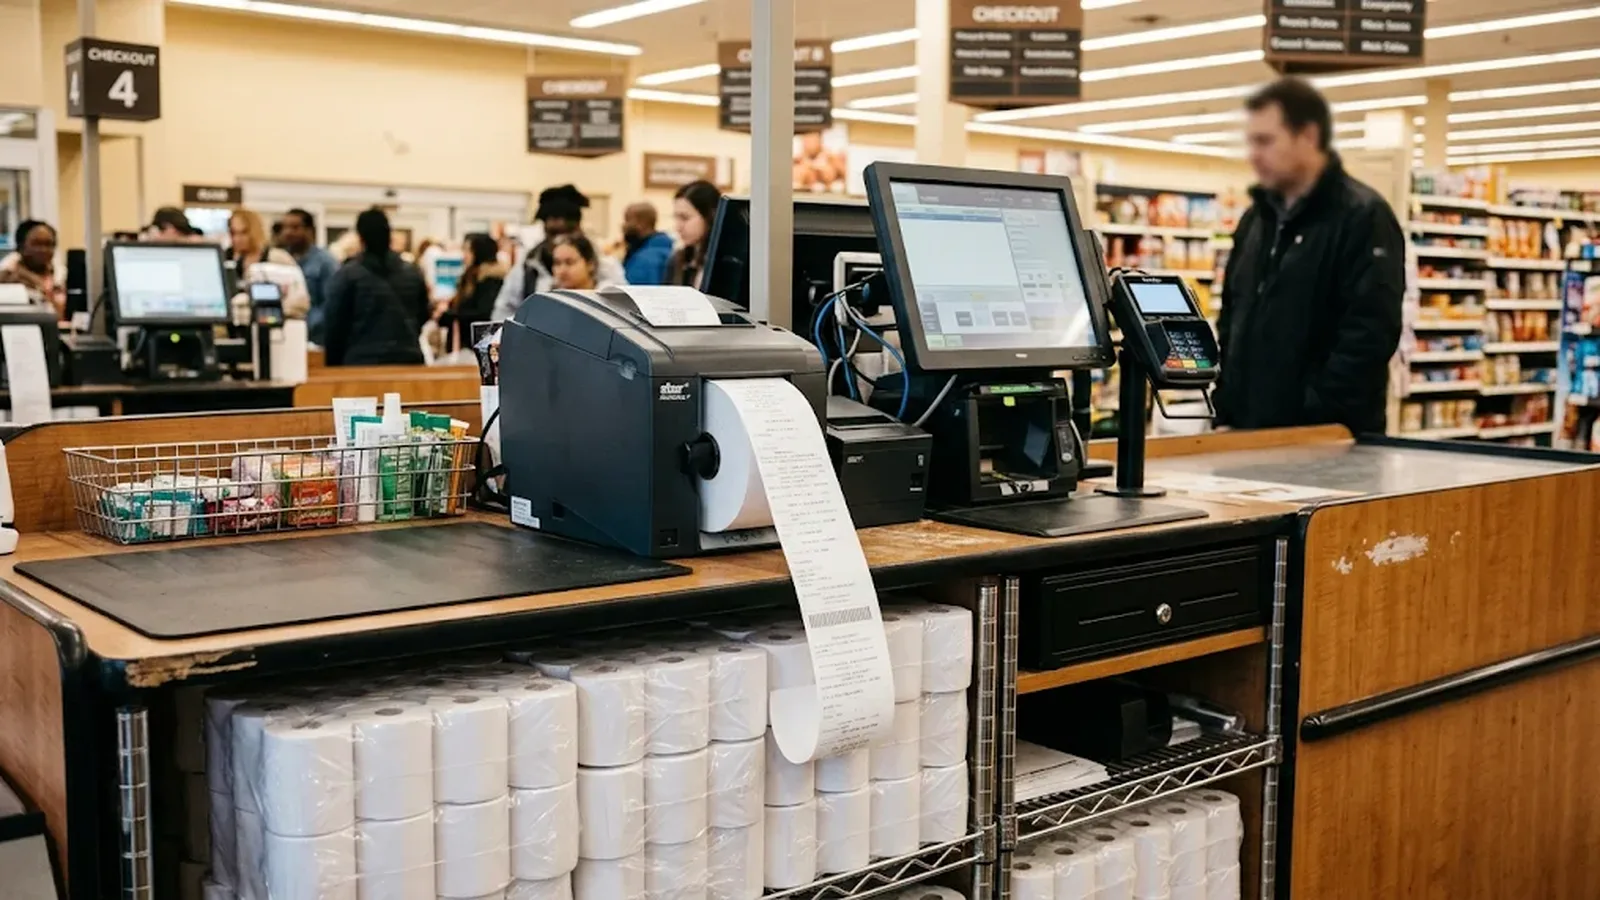
A 3 1/8 thermal paper roll is the inch-format receipt roll class that dominates North American point-of-sale duty — 3.125 inches of width, functionally the same 80 mm class that metric markets specify, wound on a small core and cut to a roll diameter the device's paper bay accepts. The class splits into sub-formats by roll length: 3 1/8 x 220, 3 1/8 x 230 and longer x273 variants, where the second number is the roll's diameter in feet-derived units. What separates a reliable supply programme from a stream of misfeeds is specification discipline — width held to ±0.5 mm, core and wall controlled, outside diameter matched to the device fit chart, basis weight stated per grade, and a developer class documented with COA and SDS per batch.
Walk into a coffee chain, a pharmacy or a big-box checkout in the United States or Canada and the receipt paper behind the counter is almost certainly the same class of product: a 3 1/8 thermal paper roll, three-and-one-eighth inches wide, imaged by a direct thermal print head with no ribbon and no ink. The format survived the transition from impact registers to thermal receipt printers because its width matches the standard receipt layout — enough for logos, itemised lines and mandates like tip lines — while staying narrow enough for compact paper bays.
The inch framing trips up international buyers. A 3 1/8 paper roll is not a different product from an 80 mm roll; it is the same 80 mm class expressed in US customary units, and the two specifications must reconcile exactly — because a millimetre is wider than an eighth of an inch, an 80 mm roll will not feed a path slit for 3.125 inches. which decides metres per roll and how often the device is opened. Sub-formats add another layer: 3 1/8 x 220, 3 1/8 x 230 and longer x273 variants differ in roll length — the second number is feet of paper per roll — which decides metres per roll, change frequency at the counter and carton economics.
Procurement teams standardising on one supplier can review our POS and receipt paper rolls alongside the comparisons in this guide, where inch and metric designations are documented against the same measured geometry before a fleet-wide order is placed.
This guide covers what the 3 1/8 class actually names, the sub-format landscape inside it, the specifications that decide feed and image behaviour, and the commercial terms that matter when the class is bought at manufacturing scale for North American fleets.
- 3 1/8 inches is the imperial expression of the 80 mm receipt class — quote the exact decimal (3.125 in / 79.38 mm class) and reconcile it with the device fit chart, not with a rounded number.
- The class splits by roll length, not width: 3 1/8 x 220, x230 and x273 carry roughly 67, 70 and 83 metres per roll, trading change frequency against paper-bay clearance and carton economics.
- Width tolerance at the roll edge is the feed-critical dimension — ±0.5 mm, verified by in-line gauging at slitting, prevents binds and false end-of-life readings.
- Match grade to duty: lightweight 48–55 gsm stock maximises metres and feeds fast; heavier grades buy durability where receipts are handled, filed or exposed to heat.
- Buying from a coating-and-converting mill gives the inch class what a distributor cannot: batch COA and SDS documentation, controlled diameter from core to OD, and export packing that survives the ocean leg.
What the 3 1/8 class actually names
The specification '3 1/8' is a width statement: three and one-eighth inches, or 3.125 inches, which converts to 79.38 mm. North American receipt hardware is designed around this width class, and the industry continues to quote it in inches even as the underlying manufacturing is done in millimetres — thermal substrate is coated and slit on metric equipment, then sold into an inch-defined market. That conversion seam is where buying errors live: a buyer who specs '80 mm' for hardware that wants 3 1/8 inches receives rolls one tenth of a millimetre too wide for the guides, and the complaint surfaces as intermittent binds that no service call resolves.
The second number in formats like 3 1/8 x 230 is not a metric width or a diameter — it is the roll's length in feet, a legacy of the North American market: 230 feet is roughly 70 metres of paper on the roll, and x220 or x273 variants shorten or extend that to about 67 and 83 metres. What matters operationally is the physical outcome: longer rolls hold more metres per roll, reduce change frequency at the counter, and produce a larger outside diameter that must still clear the device's paper bay and lid. Sub-formats inside the class — x220, x230, x273 — exist precisely because different devices tolerate different diameters, and a fleet with mixed hardware may run two or three sub-formats of the same width. Outside diameter is therefore an output of length, grammage and caliper — and it still needs to be held batch to batch, because silent diameter creep is the quietest way a repeat order degrades.
Geometry therefore travels as a set, never as a single number: width, core inner diameter and wall, outside diameter, and winding hardness. Each has a tolerance, each is measurable at goods-in, and each fails differently in the mechanism.
| Parameter | Typical class value | Why it matters |
|---|---|---|
| Width | 3.125 in (79.38 mm class), slit ±0.5 mm | Guide clearance; jam-free feeding |
| Core ID / wall | 12.7 mm (1/2 in) class, wall ≥0.8 mm | Spindle fit; first-revolution feed |
| Roll length (sub-format) | 220 / 230 / 273 ft (≈67 / 70 / 83 m) | Metres per roll; change frequency |
| Basis weight | 48–75 gsm per grade selection | Metres per roll; stiffness; durability |
| Winding | Hard, consistent tension, no telescoping | Transit stability; sensor accuracy |
| Developer class | BPA-free or phenol-free, named on the sheet | Compliance documentation chain |
Specifications that decide feed and image behaviour
Width is the first feed-critical dimension, and the inch-to-metric seam makes it doubly so. The roll edge must be clean — a burr or crushed edge reads as a false end-of-paper to the sensor or sheds dust into the path. Professional suppliers gauge width in-line at slitting rather than sampling finished rolls, and can show a setup record from a recent production run. Ask for the measurement method, not just the tolerance.
Core and outside diameter govern loading and run time. A soft core collapses under the spindle latch; an oval core misfeeds on the first revolution; diameter that creeps upward between orders slowly overfills paper bays across a fleet. Basis weight and caliper then decide how many metres fit in the diameter and how the paper behaves under the print head — lightweight grades around 48–55 gsm maximise metres and feed easily in compact paths, while heavier stock trades metres for stiffness where receipts survive in a till drawer for weeks. Where a programme needs several formats from one supplier, our custom thermal paper programme covers width, core, roll diameter and developer class in a single specification sheet, so mixed sub-format fleets run on one documented standard.
Image behaviour completes the set. Print density should be quoted with the measurement — a densitometer target tied to the developer system in use — because density drift between batches is invisible until a scanner or a human eye complains. The table above is the minimum sheet a buyer should demand per SKU; anything less is catalogue vocabulary.
Grade and developer choices for North American duty
Grade selection in the 3 1/8 class tracks duty, not fashion. High-volume quick-service counters that print short, dense receipts favour lightweight grades for metres per roll and fast feeding; pharmacy and general retail where receipts are filed or survive in a till drawer justify heavier stock; hospitality and drive-thru environments that expose paper to grease, condensation and heat need top-coated constructions, because a bare thermal surface loses its image to the same chemistry that develops it.
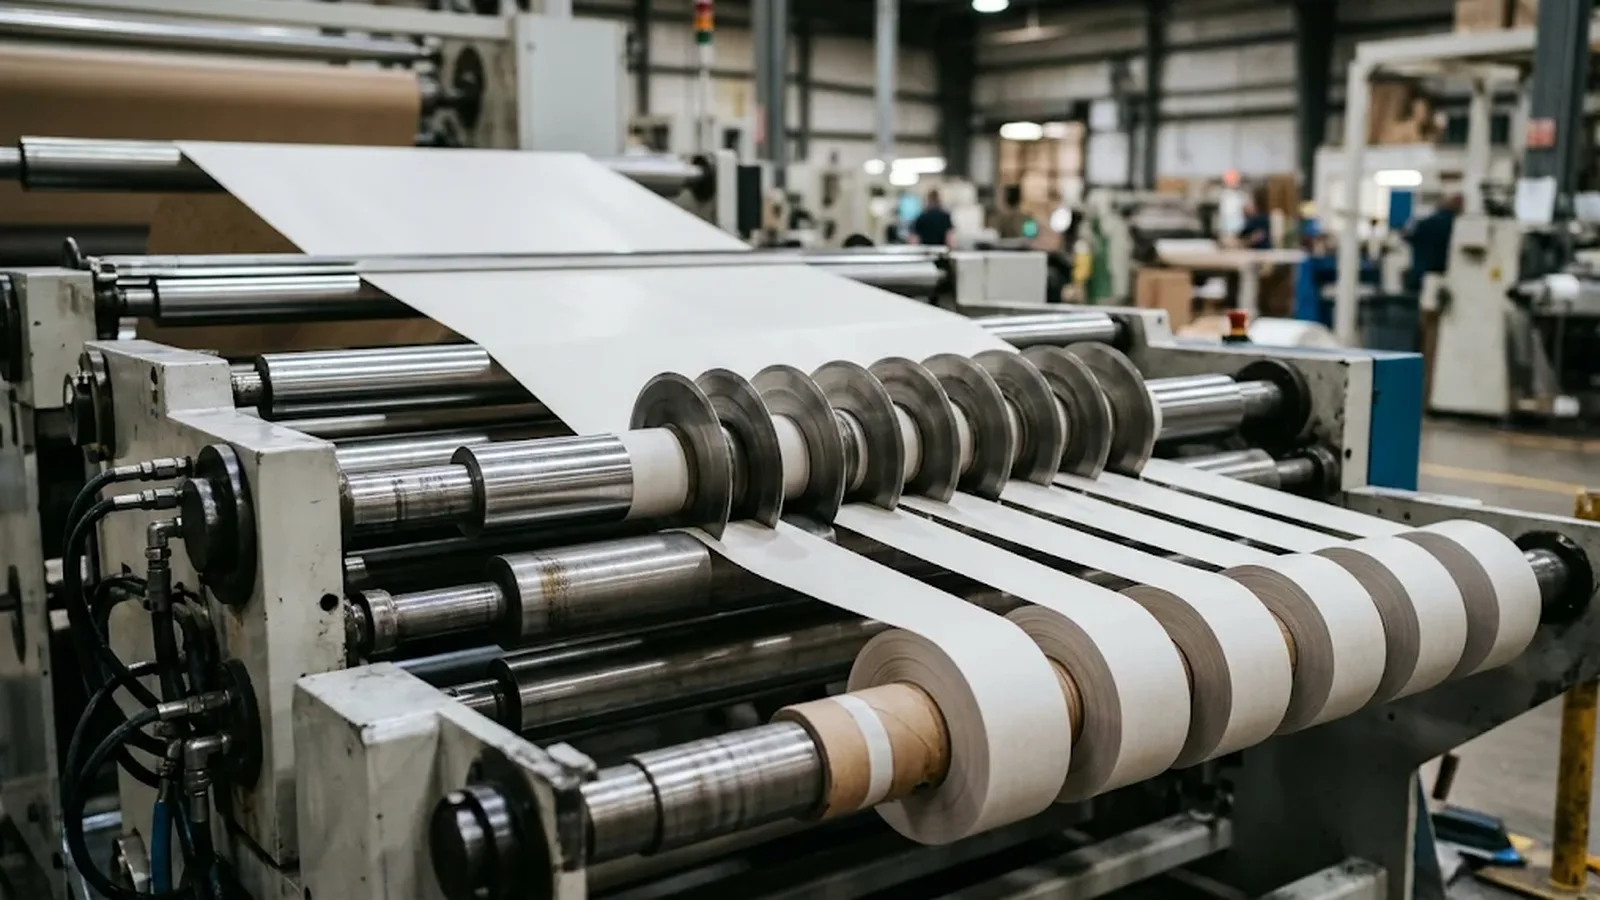
Developer chemistry is now a purchase condition in North American retail. Chain compliance teams specify BPA-free as a floor and phenol-free constructions where regulation or customer policy requires it. The buyer's protection is documentation: the developer system named on the specification sheet, a COA and an SDS identifying the sensitizer chemistry with every batch. A mill with its own coating line produces that chain directly; a trader forwards it, and the seams show when an audit asks a question the middleman cannot answer.
Fleet standardisation benefits most from grade discipline: one density target, one developer class, one grade ladder across every device in the estate, so a receipt printed in one store reconciles identically with one printed in another.
Buying the class at manufacturing scale
The 3 1/8 class is a high-rotation consumable, and the commercial structure should be judged on the tenth order, not the first. MOQ should be stated per sub-format, driven by slitting setup and carton configuration; lead time should reconcile with the coating schedule rather than with hope; price validity should be credible against the supplier's own coating economics. Print programmes — a logo or promotional line added during converting — need artwork revision control so a design never changes silently between batches.
Freight economics favour the lightweight end of the class: lighter grammage means more metres per tonne and more rolls per container, which is why the yield conversation belongs in the quotation, not after it. Requests that combine several formats can be quoted together; see 48 gsm lightweight thermal paper for the yield and freight logic behind the lighter receipt grades that dominate high-volume inch-format fleets.
Packing decides what arrives. Rolls are hygroscopic, and a carton that crosses an ocean without moisture-barrier wrapping and desiccant can arrive as a different product than the one sampled. Where image life and construction drive the grade decision, our top-coated vs non top-coated guide compares the two constructions on retention, cost and machine behaviour, so the choice is made per environment rather than per catalogue.
Programme shorthand: width 3.125 in ±0.5 mm, core and OD per sub-format, grade and caliper stated, density target quoted with method, developer class documented per batch, MOQ and lead time per format, moisture-barrier export packing.
Frequently asked questions
Is a 3 1/8 thermal paper roll the same as an 80 mm roll?
Functionally yes, dimensionally no. 3.125 inches converts to 79.38 mm, so an 80 mm roll is about 0.6 mm wider and can bind in hardware designed for the inch class. Quote the exact decimal your device documentation uses and hold the supplier to that width with a ±0.5 mm tolerance.
What do the numbers in 3 1/8 x 230 mean?
The first number is the roll width in inches; the second is the roll length in feet — 230 feet is roughly 70 metres of paper on one roll. Larger second numbers mean more metres per roll and fewer paper changes, at the cost of a larger outside diameter that must still clear the device's paper bay. Mixed fleets may legitimately run several sub-formats of the same width.
Which paper grade should I choose for the 3 1/8 class?
Match grade to duty: 48–55 gsm for high-volume counters that want metres per roll and fast feeding; heavier grades where receipts are handled, filed or exposed to heat; top-coated constructions for grease, moisture and abrasion environments such as kitchens and drive-thru windows. State caliper with a tolerance and verify it at goods-in.
Are BPA-free 3 1/8 rolls available at wholesale scale?
Yes. BPA-free is the mainstream specification for new programmes, and phenol-free constructions are available where policy requires them. Insist that the developer system is named on the specification sheet and that each batch ships with a COA and SDS, so the compliance chain survives audits.
What MOQ should I expect for inch-format receipt rolls?
Expect MOQ stated per sub-format, driven by slitting setup and carton configuration rather than a blanket number. Mixed-format programmes can usually consolidate several roll sizes into one production slot and one container; a supplier who cannot state MOQ and lead time per format is a broker risk.