
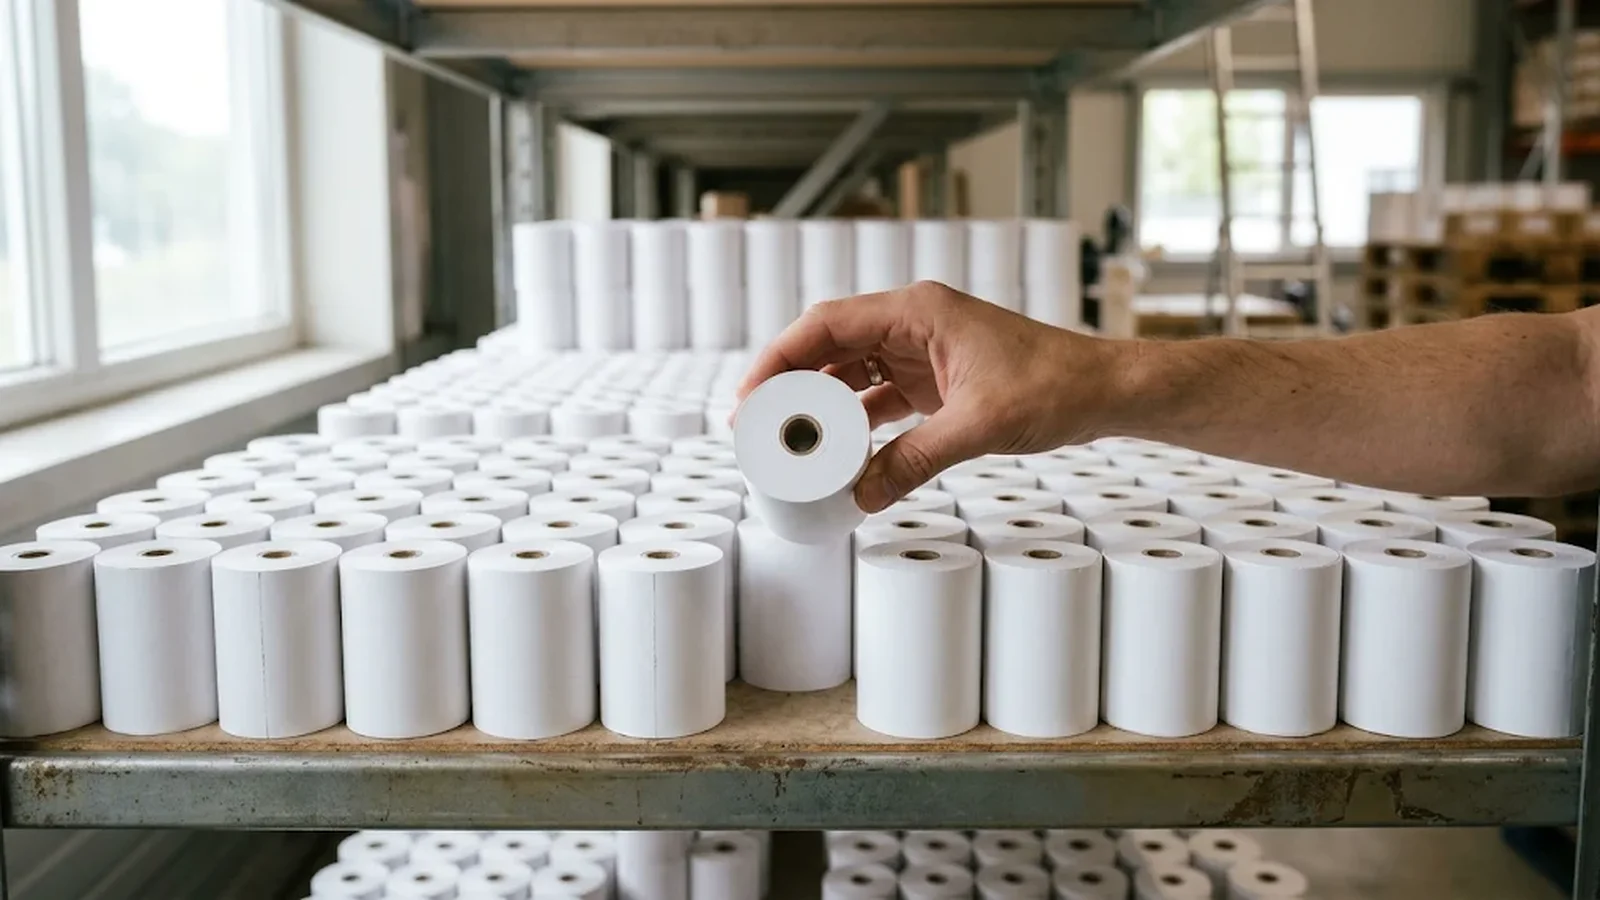
A 57x38 thermal paper roll is 57 mm wide with a 38 mm outside diameter — the short-diameter member of the 57 mm family, typically carrying 12–14 metres of 55–58 gsm direct thermal stock on a 10 mm or 12.7 mm core. It is specified for compact mechanisms whose roll cavity cannot accept the taller 57x40, 57x50 or 57x60 spools: mini receipt printers, compact card terminals, handheld delivery devices and pocket EDC hardware. Buying it correctly means specifying the full geometry — width, core, OD, wind direction and gsm — not just '57 mm paper', because the 38 mm diameter is exactly what the mechanism was designed around. Oversized rolls bind; undersized ones defeat the end-of-life sensor. Source the format from a converter who slits to ±0.5 mm width tolerance and validates diameter against the device fit chart, and standardise the core and winding across the programme so every roll feeds identically.
The 57 mm width family dominates compact thermal printing worldwide, but it is the diameter — not the width — that decides whether a roll works in a given device. Within this family, the 57x38 thermal paper roll is the short-roll class: roughly 12–14 metres of stock wound to a 38 mm outside diameter, built for the smallest cavities in the market. It feeds mini printers, compact card terminals, pocket EDC devices and the handheld hardware used across delivery, field service and queue-busting retail.
The commercial problem is that the format is often ordered as generic '57 mm paper'. A distributor that ships 57x40 or 57x50 rolls against a 57x38 specification will hear about it immediately: the taller spool binds in a cavity cut for 38 mm, and the complaint lands on the supplier. Precision in this class is not cosmetic — it is the difference between a repeat order and a returned pallet.
Buyers comparing these specifications can review our POS and receipt paper rolls, where each roll class is documented by width, core, outside diameter and grade before an order is placed.
This guide covers the geometry of the 57x38 class and where it fits against the taller 57 mm diameters, the metre-yield and roll-count arithmetic buyers should run before quoting, gsm and coating selection for the compact format, the manufacturing tolerances that decide feed reliability, and the sourcing structure — MOQ, packing, specification discipline — that keeps a 57x38 programme trouble-free at volume.
- 57x38 means 57 mm width, 38 mm outside diameter — the short-diameter 57 mm class carrying roughly 12–14 m of stock; it is not interchangeable with 57x40, 57x50 or 57x60 formats.
- Specify the full geometry on the purchase order: width, core (10 mm or 12.7 mm), OD, wind direction and gsm — cavity fit is decided by all five, never by width alone.
- 55–58 gsm stock is the mainstream for this class; lighter stock maximises metre yield but can compromise feed stiffness in short mechanisms.
- Width tolerance of ±0.5 mm and a hard, evenly wound roll are the two manufacturing details that separate jam-free 57x38 supply from complaint-generating supply.
- Distributors should list the format as its own SKU with a per-device fit chart: the 57 mm family's diameters are the most commonly confused consumable specification in compact printing.
What 57x38 actually specifies: geometry before everything
Read the format as width x outside diameter. The 57 mm width is nominal — usable print width runs 48–54 mm depending on the mechanism — and the 38 mm outside diameter is the constraint the device cavity was engineered around. Between the core and the OD sits the working stock: a 57x38 roll on a 10 mm core holds about 13–14 metres of 55 gsm paper; on a 12.7 mm core the same OD holds nearer 12 metres. Two rolls with identical box prints can therefore differ by more than 15% in delivered length — which is why the core belongs on the specification line.
Against its siblings, the class positions clearly. 57x40 adds a metre or two of stock and is the most common compact-terminal diameter; 57x50 is the mid-length card-terminal format; 57x60 and taller serve countertop devices that reward fewer changes. The 38 mm class exists because some mechanisms — pocket EDC hardware, early compact printer designs, mini label-and-receipt hybrids — have no room for anything taller. Fleet buyers should treat the diameters as separate SKUs from day one: the single most common 57 mm misorder is a 40 mm spool supplied against a 38 mm cavity.
Wind direction completes the geometry. Paper-out-front and paper-out-back rolls are both sold in the width family, and a reversed wind renders a dimensionally perfect roll useless — the print head receives the back of the stock. The wrapper rarely signals the wind, so the specification sheet must state it explicitly and the packing must preserve it.
Where a programme needs several 57 mm diameters from one supplier, our custom thermal paper programme covers width, core, roll diameter and developer class in a single specification sheet, so the whole compact-format range can be quoted and supplied under one agreement.
Metre yield and roll-count maths for buyers
Volume buyers in this class think in receipts per roll and rolls per device per month. A 13-metre 57x38 roll yields roughly 90–110 short transaction slips at typical compact-printer receipt lengths of 120–150 mm. Multiplying daily transactions by device count converts the format into a monthly roll forecast — and exposes the true cost metric: cost per receipt, not price per roll.
That arithmetic also disciplines quote comparison. A slightly cheaper 57x38 roll on a fatter core delivers fewer metres per diameter, quietly raising cost per receipt; a lighter gsm stretches yield but can trade away feed stiffness. Buyers comparing quotes should normalise three numbers — metres per roll, receipts per metre, and price per roll — into a single cost-per-receipt figure before ranking suppliers.
Distributor economics matter here too. The 57x38 class is high-unit-count, low-cube stock: a carton holds dozens of rolls, a pallet holds hundreds, and shelf-life is measured in years when the stock is stored correctly. Buyers consolidating several compact formats into one shipment should confirm the packing spec — carton count, pallet pattern, moisture barrier — at quote stage, because repacking after arrival erodes exactly the margin the consolidation was meant to protect.
For production volumes, the same construction logic applies to our 48 gsm lightweight thermal paper, quoted per jumbo roll, slit reel or finished format, where basis weight and yield are documented per grade before an order is placed.
Gsm and coating choice inside a short cavity
Basis weight behaves differently in a 38 mm-diameter roll than in a tall one. Because the winding length is short, the caliper of the stock has an outsized effect on delivered metres: a 58 gsm stock yields noticeably less paper per roll than 55 gsm at the same OD — proportionally more than buyers expect from taller formats. The mainstream class is 55–58 gsm; programmes that maximise roll capacity choose the lighter end, and programmes that need stiffness for reliable feeding in mini mechanisms stay at the heavier end.
Coating selection follows the receipt's life, and the receipt's life in compact devices is usually short but public. Slips from mini printers and compact terminals land in pockets, door pockets of delivery vans and customers' hands, so friction and wallet heat attack an untopcoated image quickly. Top-coated construction holds scan-grade contrast through that life and is the standard recommendation for card-terminal and customer-facing 57x38 programmes; untopcoated stock remains the honest cost choice where the print is reconciled, photographed or filed the same day it is printed.
Sensitivity rounds out the grade decision. Compact and handheld devices manage battery and head energy tightly, so a stock matched to the mechanism's energy window prints full density at speed and keeps cold-morning prints legible; a sluggish coating forces higher energy and faint images. Validation on the actual device — not a datasheet comparison — is the only reliable test, and it takes a handful of sample rolls.
Where image life is the deciding factor, our top-coated vs non top-coated guide compares the two constructions on retention, cost and machine behaviour.
| Format | Typical yield (55–58 gsm) | Core | Typical duty |
|---|---|---|---|
| 57x38 | ≈12–14 m | 10 mm / 12.7 mm | Mini printers, compact and pocket terminals, handheld devices |
| 57x40 | ≈14–18 m | 10 mm / 12.7 mm | The most common compact card-terminal diameter |
| 57x50 | ≈19–21 m | 12.7 mm | Mid-length terminal format for fewer changes |
| 57x60+ | ≈25 m and up | 12.7 mm | Countertop devices with tall cavities |
Manufacturing tolerances that decide feed reliability
In a short-diameter class, small manufacturing errors are proportionally large. Width tolerance should be held to ±0.5 mm: a roll slit wide jams at the paper-path guide, a roll slit short leaves a gap the mechanism reads as end-of-life. Diameter should be wound to the stated OD, because cavity clearance in compact hardware is measured in fractions of a millimetre.
Winding quality is the second discriminator. A hard, even wind keeps the roll round on the spindle; a soft or telescoped wind produces oval rolls that wobble at speed, fling the leading edge out of the sensor path and generate the classic 'random jam' complaint that no single roll can reproduce in the office. Edge condition matters as well — burrs or a crushed edge from poor slitting shed dust into compact mechanisms that are rarely cleaned.
End-of-life behaviour completes the reliability picture. The 38 mm class feeds devices whose low-paper sensors trigger on diameter or on transmitted light through the roll core area; consistent winding ensures the sensor reads the true state of the roll rather than a winding artefact. This is why a converter running the same core, tension and tolerance across the whole programme delivers fewer complaints than a trader assembling rolls from several mills — the mechanism sees one consistent product, shift after shift.
Buyers standardising a compact-format programme can shortlist on these three controls — width tolerance, winding hardness and sensor-consistent finishing — then confirm the rest on machine trials. Everything else on the datasheet is secondary to whether the roll simply feeds, every time, in the fleet it was bought for.
Order-line shorthand that prevents most 57x38 complaints: '57 mm x 38 mm OD, core [10/12.7] mm, wind [front/back], 55–58 gsm, top-coated, BPA-free developer, width tolerance ±0.5 mm — matched to [device family] fit chart.'
Frequently asked questions
What is a 57x38 thermal paper roll used for?
It is the short-diameter 57 mm format for compact mechanisms: mini receipt printers, pocket and handheld card terminals, delivery and field-service devices, and other hardware whose roll cavity is engineered around a 38 mm outside diameter. It is not a substitute for 57x40, 57x50 or taller formats — cavity fit fails with even a few millimetres of extra diameter.
How many metres of paper are in a 57x38 roll?
Typically 12–14 metres of 55–58 gsm stock, depending on core size and exact caliper — about 13–14 m on a 10 mm core and nearer 12 m on a 12.7 mm core at the same 38 mm OD. Confirm measured metre length per roll with the supplier rather than relying on nominal claims.
Is 57x38 the same as 57x40?
No. Both are 57 mm wide, but the outside diameters differ by 2 mm, which is enough to bind in a cavity cut for the 38 mm class. The two formats are the most commonly confused SKUs in the 57 mm family and should always be listed and ordered as separate items with their own fit charts.
What gsm should 57x38 rolls be?
The mainstream class is 55–58 gsm. Lighter stock maximises metre yield in the short diameter; heavier stock improves feed stiffness in mini mechanisms. Because the roll is short, caliper changes have a proportionally large effect on delivered metres — fix the gsm and tolerance on the specification line.
What should I specify when sourcing 57x38 rolls at volume?
Specify width (57 mm, ±0.5 mm tolerance), outside diameter (38 mm), core size, wind direction, gsm class, coating (top-coated for customer-facing programmes) and developer class (BPA-free or phenol-free), and match the whole set to the device family's fit chart. Ask the supplier to hold the same core, winding and tolerances across the programme so every roll feeds identically.