
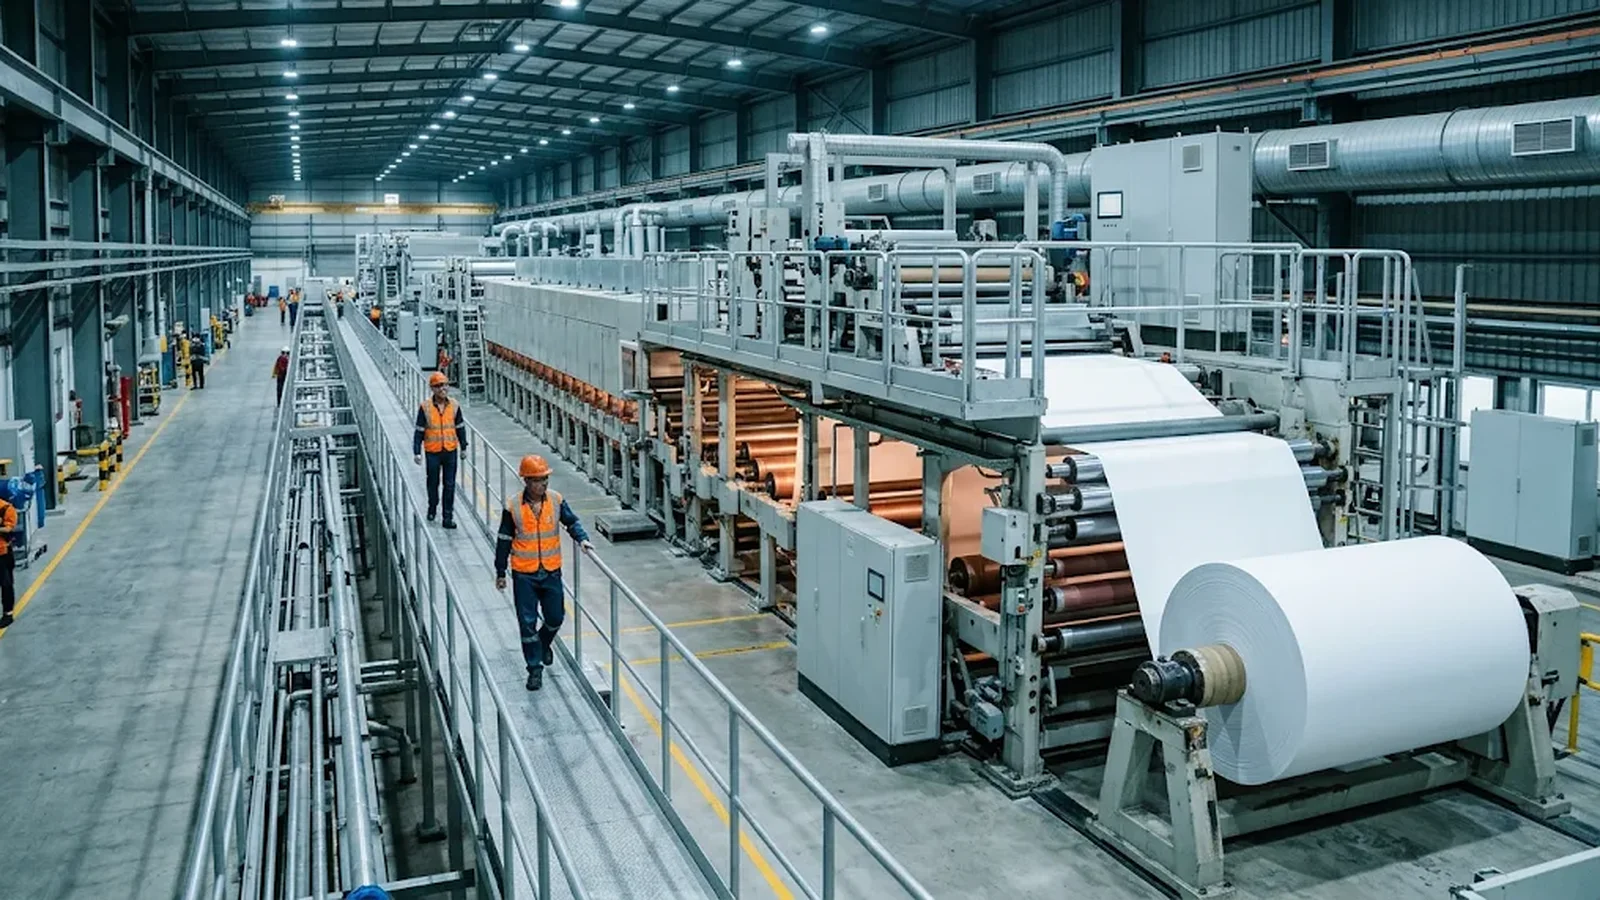
China produces the majority of the world's thermal paper, and the gap between a successful import programme and an expensive lesson comes down to qualification: verifying that the counterparty actually coats paper, that its laboratory measures what the datasheet claims, that its compliance dossier (SDS and COA per batch, REACH-supporting developer documentation, chain-of-custody for the base paper) is issued by the producing plant rather than forwarded, and that its export operation can load, document and deliver a container predictably. Importers should qualify on evidence — coating-line and converting equipment lists, completed inspection records, sample rolls from the actual production build, factory audit (remote or on-site) — and structure commercial terms so risk transfers correctly: realistic MOQ and lead time against the coating schedule, payment terms matched to order maturity, and packing specified as part of the product. A thermal paper manufacturer that coats its own jumbo stock can sign one specification from chemistry to carton; a trader structurally cannot, and the difference appears in every repeat order.
Importers arrive at China's thermal paper industry with a price advantage and a verification problem. The category is crowded with companies describing themselves as manufacturers, factories and mills — some coat their own paper, some convert jumbo bought from coaters, some do neither and trade. The vocabulary is identical; the capability is not. Qualifying a thermal paper manufacturer in China is therefore not a price negotiation but an evidence exercise, run before the first purchase order is signed.
The economics justify the effort. A coating manufacturer selling direct removes one or two margins from the chain, controls the tolerance story from chemistry to carton, and can support compliance questions from the production record rather than from a supplier's email. But those advantages only materialise when the factory is what it claims — and the verification methods are well within reach of any serious importer.
Our thermal paper jumbo rolls programme publishes the coating and converting test data behind each width and grade, so specification claims can be verified against the mill's own measurements rather than a catalogue line before an import programme is committed.
This guide sets out the qualification sequence importers actually use: verifying manufacturing identity, reading capacity and laboratory signals, building the compliance dossier, running a sampling protocol that de-risks first orders, and structuring Incoterms, payment and container planning so the programme survives contact with real logistics.
- Verify manufacturing identity first: a coating manufacturer owns a thermal coating line and can name its machines, widths and daily capacity; a trader cannot, and the equipment conversation exposes the difference quickly.
- The laboratory is the factory's honesty signal: ask for completed inspection records — basis weight, caliper, image density, sensitivity — not certificates of generic compliance.
- Build the compliance dossier per batch: SDS identifying the developer chemistry, COA from the producing plant, REACH-supporting documentation, and chain-of-custody for base paper where policy requires it.
- De-risk the first order with a written sampling protocol: samples from the actual production build, tested on the buyer's own printers and devices against agreed acceptance numbers.
- Structure trade terms deliberately: Incoterms matched to the buyer's logistics capability, payment maturity matched to production milestones, and moisture-barrier packing specified as part of the product.
Verifying manufacturing identity: coater, converter or trader
The first qualification question is blunt: does this company coat thermal paper, or does it buy and resell? The answer is verifiable without a site visit. A coating manufacturer describes its coating line concretely — machine type, coatable width range, annual or daily capacity, the grades it runs — and its staff discuss developer systems, coat weights and sensitivity classes with the fluency that only production experience gives. Ask for the equipment list and the production schedule for your target widths; vague answers, or a 'factory' that pivots the conversation to price, are diagnostic.
Converting capability is the second axis. Many strong suppliers coat and convert under one roof — slitting jumbo stock to customer widths, rewinding to specified cores and diameters, printing and packing. Others coat only and sell jumbo; others only convert. None of these is disqualifying, but each changes what the supplier can promise: a full-line manufacturer can hold width, grade and packing in one specification and one traceability chain, while a converter buying jumbo from third parties inherits someone else's chemistry variability. Ask which parts of the chain are in-house and which are purchased, then ask who signs the specification covering the whole.
Export competence is the third identity marker, and the easiest to test. A manufacturer that ships containers routinely will quote Incoterms fluently, describe its nearest port and container loading process, and produce export packing specifications without prompting. A trading intermediary improvises this conversation. The distinction matters because an import programme's landed cost and risk profile are set as much by the export operation as by the paper mill.
Buyers consolidating formats across an import programme can review our custom thermal paper programme, which documents width, core, roll diameter, developer class and packing in a single specification sheet — the structure a qualified China manufacturing partner should be able to sign.
Capacity and laboratory signals that separate real mills
Capacity claims are cheap; capacity evidence is not. Useful signals include the machine list with coatable widths and speeds, current utilisation against known customers' volumes, and a production calendar that can name a realistic slot for a trial order. A thermal paper factory in china running its own coating line can usually schedule a pilot within weeks; an intermediary must ask someone else, and the lead time honesty of the first quotation predicts the reliability of every later one.
The laboratory is the strongest signal of all. Ask for a completed inspection record from a recent batch — basis weight, caliper, brightness, smoothness, image density and sensitivity, with test methods named. Real laboratories produce records that look like working documents: per-shift readings, batch numbers, operator initials. Certificates that arrive as glossy PDFs with no batch traceability are marketing, and the difference between the two is exactly the difference between a repeat order that conforms and one that quietly drifts.
Tolerance ownership completes the technical audit. Every quoted specification should carry a tolerance and a measurement method: width ±0.5 mm on receipt classes, caliper per grade with a stated band, image density against a densitometer reading, roll diameter and core within the device fit chart. A manufacturer that quotes tolerances per property and explains how each is measured is telling you how it runs its plant. One that quotes 'high quality' without numbers is asking you to accept risk it has not priced.
| Signal | Coating manufacturer | Trading intermediary |
|---|---|---|
| Equipment talk | Names coating/slitting machines, widths, capacity | Speaks in product categories, pivots to price |
| Inspection records | Working documents with batch numbers and methods | Glossy certificates without traceability |
| Compliance dossier | SDS/COA issued by the producing plant | Forwarded, often untranslated |
| Lead time | Scheduled against the coating calendar | Estimated, then renegotiated |
| Specification signing | One document, chemistry to carton | Disclaims chemistry 'per mill' |
The compliance dossier importers should demand
Thermal paper imports are document-intensive, and the burden scales with the destination market. The baseline set travels with every batch: a commercial invoice and packing list that match the cartons, a bill of lading, and — product-specific — an SDS identifying the developer chemistry and a COA from the producing plant tying the batch to its test results. Importers into regulated retail channels add REACH-supporting documentation for the developer system, food-contact declarations where receipts touch food packaging, and chain-of-custody certificates for base paper where sustainability policy requires them.
The qualification point is who issues the documents. A plant that coats its own paper generates its SDS and COA from production records and can defend them in an audit; an intermediary forwards documents of varying provenance and cannot answer follow-up questions. Ask, during qualification, for a sample dossier from a recent shipment — the SDS, the COA, and one batch traceability record. What arrives within 48 hours tells you how every future compliance query will be handled.
Change control belongs in the dossier too. Developer systems, coating recipes and base paper sources can change for legitimate reasons — regulation, availability, cost — but the buyer must hear about it before the container sails, not after a field complaint. A written change-notification clause, and a supplier who uses it, is worth more than any single certificate in the file.
Sampling, trade terms and container planning
Sampling is where paper qualification becomes concrete. The professional protocol: agree the specification in writing, receive sample rolls converted on the actual production line (not pilot sheets), test on your own devices against agreed acceptance criteria — image density, feeding, curl, edge quality, adhesive and liner behaviour for label constructions — and only then commit volume. Suppliers confident in their production will send production-build samples without hesitation; resistance to that request is itself a finding.
Trade terms should transfer risk where it is best managed. Ex Works and FOB suit importers with their own freight relationships; CIF hands the shipping leg to the supplier and suits buyers without logistics teams, at the price of less visibility. Payment structure should mature with the relationship — deposits balanced against completion documents at first, open terms only after repeated conformity. Price validity is a credibility test: a coating manufacturer can defend a 12-month validity from its own cost position, and a quote that expires in a week is telling you who else is in the chain.
For production volumes, the same construction logic applies to our POS and receipt paper rolls, quoted per jumbo roll, slit reel or finished format, so an import programme can phase from jumbo stock into finished formats with one partner as volumes justify converting.
Container planning is the last discipline. Mixed-format programmes consolidate several widths and SKUs into one container; pallet plans, carton compression and moisture-barrier wrapping decide what arrives after thirty days at sea. Where container loading is the next milestone in an import programme, our export shipping guide covers pallet standards, moisture-barrier packing and the document set for ocean freight.
Importer shorthand: equipment list + production schedule, completed inspection records with methods, per-batch SDS + COA from the producing plant, production-build samples with written acceptance criteria, Incoterms and payment maturity matched to order risk, moisture-barrier export packing named in the specification.
Frequently asked questions
How do I verify a Chinese thermal paper supplier is actually a manufacturer?
Ask for the equipment list — coating line type, coatable widths, capacity — and a production schedule for your target widths. Real manufacturers discuss developer systems and coat weights fluently and provide working inspection records with batch numbers. If every answer pivots to price and every certificate lacks traceability, you are talking to a trader.
What documents should accompany each thermal paper shipment?
Commercial invoice and packing list, bill of lading, and per batch an SDS identifying the developer chemistry plus a COA from the producing plant. Regulated markets add REACH-supporting documentation, food-contact declarations where relevant, and chain-of-custody certificates for base paper under sustainability policies.
What is a sensible sampling protocol before a first order?
Agree the specification in writing, request sample rolls converted on the actual production line, test on your own printers and devices against written acceptance criteria — image density, feeding, curl, edge quality — and commit volume only after conformity. Production-build samples, not pilot sheets, are the standard to insist on.
Which Incoterms suit a first import programme?
FOB suits importers with freight relationships who want control of the shipping leg; CIF suits buyers without logistics teams who prefer the supplier to manage delivery to port. Either way, specify the packing construction in the contract — moisture-barrier wrapping, carton strength, pallet plan — because packing failures surface at destuffing, far from the factory.
Can one Chinese manufacturer supply both jumbo rolls and finished formats?
Yes — manufacturers that coat and convert under one roof supply jumbo stock for further converting as well as finished receipt and label formats, and consolidate mixed widths into single containers. Confirm which parts of the chain are in-house, hold one specification sheet per SKU, and phase the programme from jumbo to finished formats as volumes justify.